4.1. Instructions
4.1.1. Making a copy of a key
The finished blank key with the milled profile is further processed on conventional key machines with due care and accuracy. Below are some tips and tricks to help you make a copy of a key:
- Shorten the blank key by cutting off the unmilled end of the key with the locating hole (e.g. using a hand-held metal saw) to the dimension depending on the key type.
- For keys with an upper limit (the so-called base), the profile length measured from the upper limit (the so-called base) should be 2-3 mm longer than the working part of the original key
- For keys without an upper limit (so-called bases), which rest on the tip of the lock, the length of the blank key profile should be 2-3 mm longer than the length of the working part of the original key
- After shortening the blank key, smooth the cut edge with a file or grinder so that the blank key is correctly positioned in the jaws of a conventional machine
- The tip of the key should be shaped so that it matches the shape of the original as closely as possible
- Pay attention to the thickness of the upper stop (the so-called base) in the original key. If the thickness of the blank key is too great in relation to the original, reduce it to the correct dimension (e.g. with a file or milling machine).
4.1.2. Special cases of key profiles
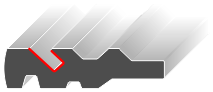
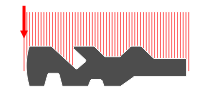
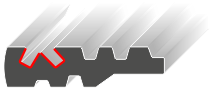
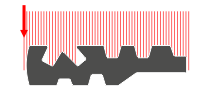
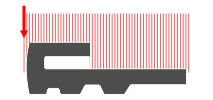
Some key profiles have a special shape that cannot be scanned and milled using a tool that is positioned perpendicular to the key cross-section (i.e., like the probe and cutter of the X-KEY Terminator machine).
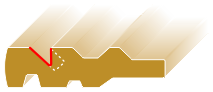
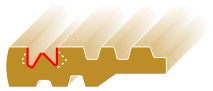
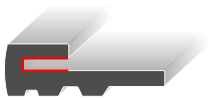
Below are some examples of key profiles that require additional processing after the standard profile milling process. The red line marks the shapes of the grooves that require special attention, i.e. how they look in the original profile in relation to the profile made on the X-KEY Terminator machine. This difference results from the scanning and milling method, as illustrated by the key profile scanning process, where you can see which areas of the profile are inaccessible to the probe.
| Original key profile | Scanning the key profile | Completed key profile |
|---|---|---|
 |
 |
 |
 |
 |
 |
 |
 |
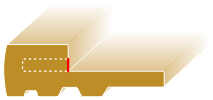 |
In such cases, the key profile requires additional processing on other machines so that the shape of the key profile matches the original. In the illustrations of the key profiles, the areas that need to be additionally milled are marked with a white dotted line. For this purpose, you can use, for example, a vertical milling machine with a suitable milling cutter. Pay particular attention to the accuracy of the additional machining, as in extreme cases the insert may be blocked by the use of an incorrectly made key.